Precision functional hardware for global OEMs
Custom-formed engine brackets, thermal heat shields, skid plates, and fluid reservoirs built to your exact CAD tolerances and production schedules.
Tolerance Standard
ISO 2768-m / ±0.05mm
Material Range
Alloy Steel, AL 5052/6061, SUS304
Production Scale
Rapid Prototypes to 50k+ Monthly
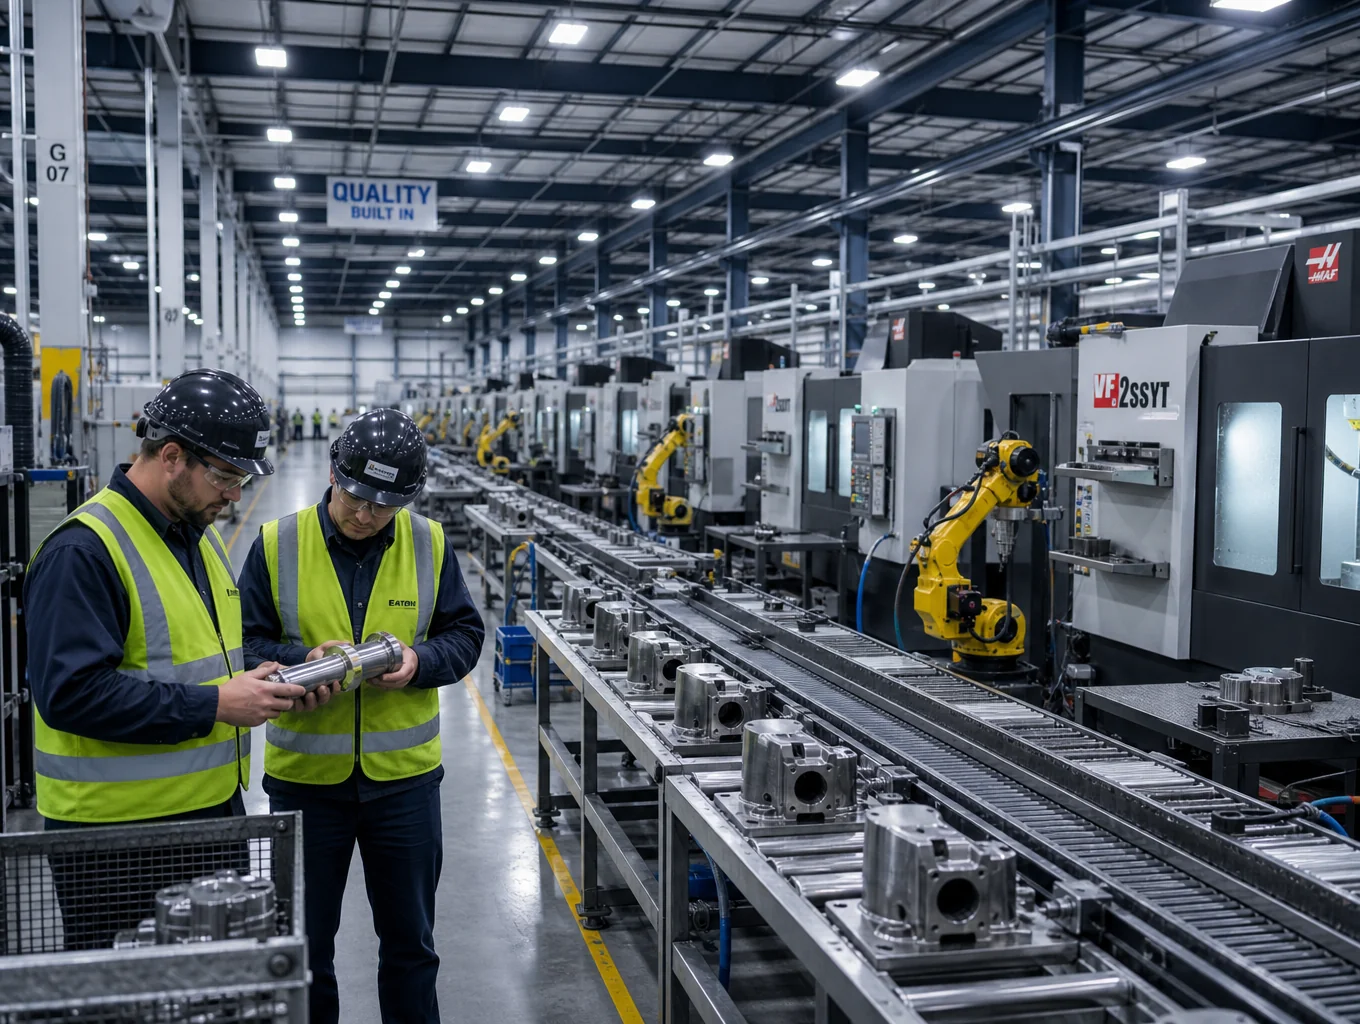
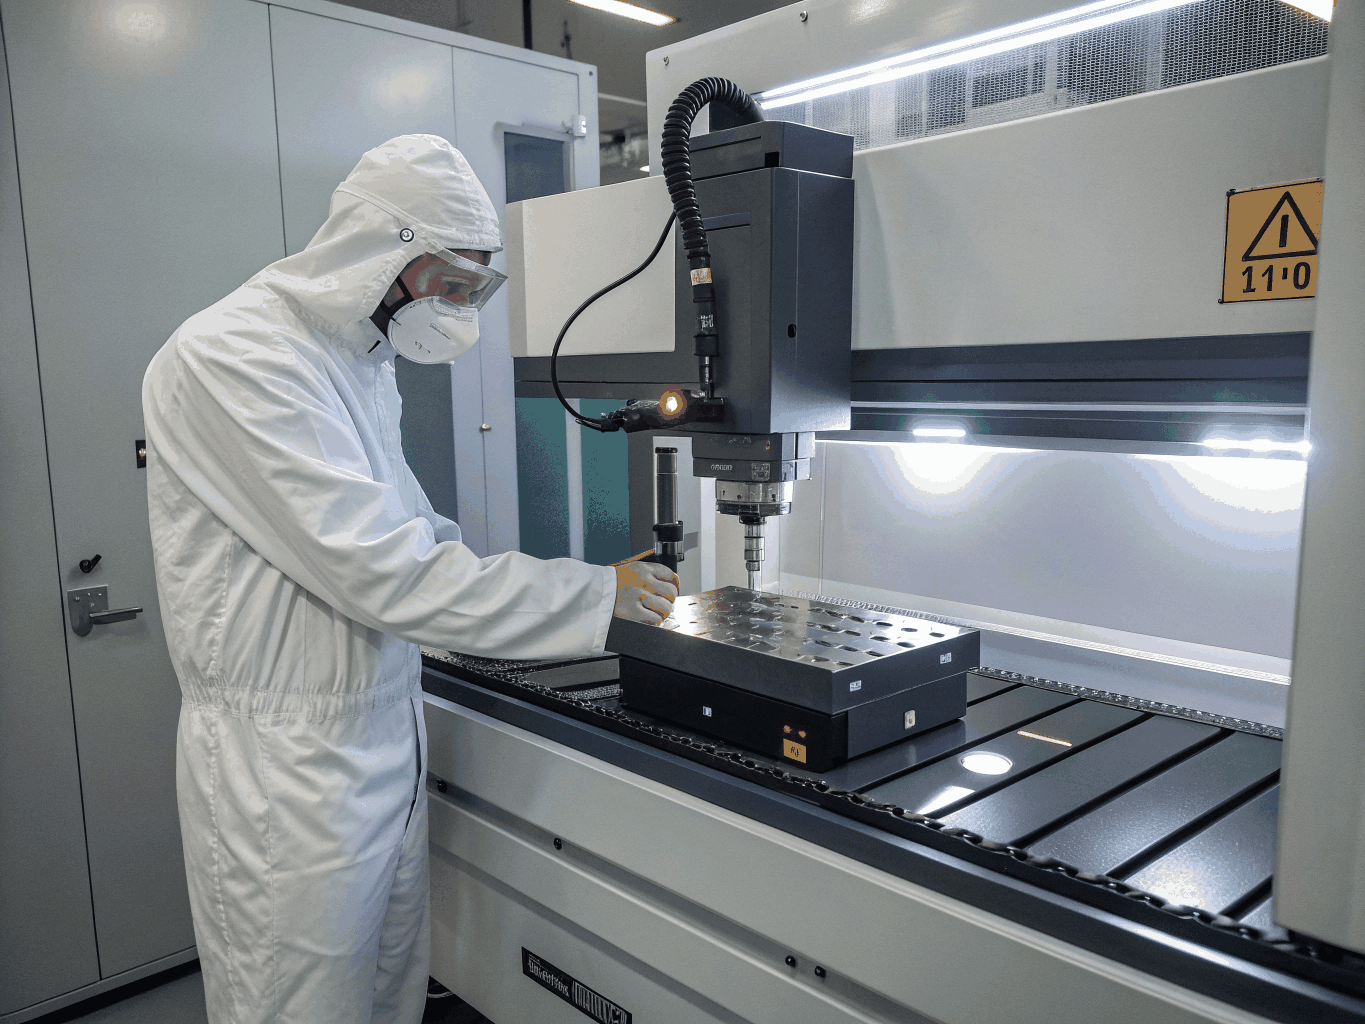
CMM Dimensional Verification
100% First-Article & In-Process Inspection
Engineered automotive components
High-precision stamped, laser-cut, and welded sheet metal assemblies built to meet strict OEM tolerance, durability, and weight reduction requirements.
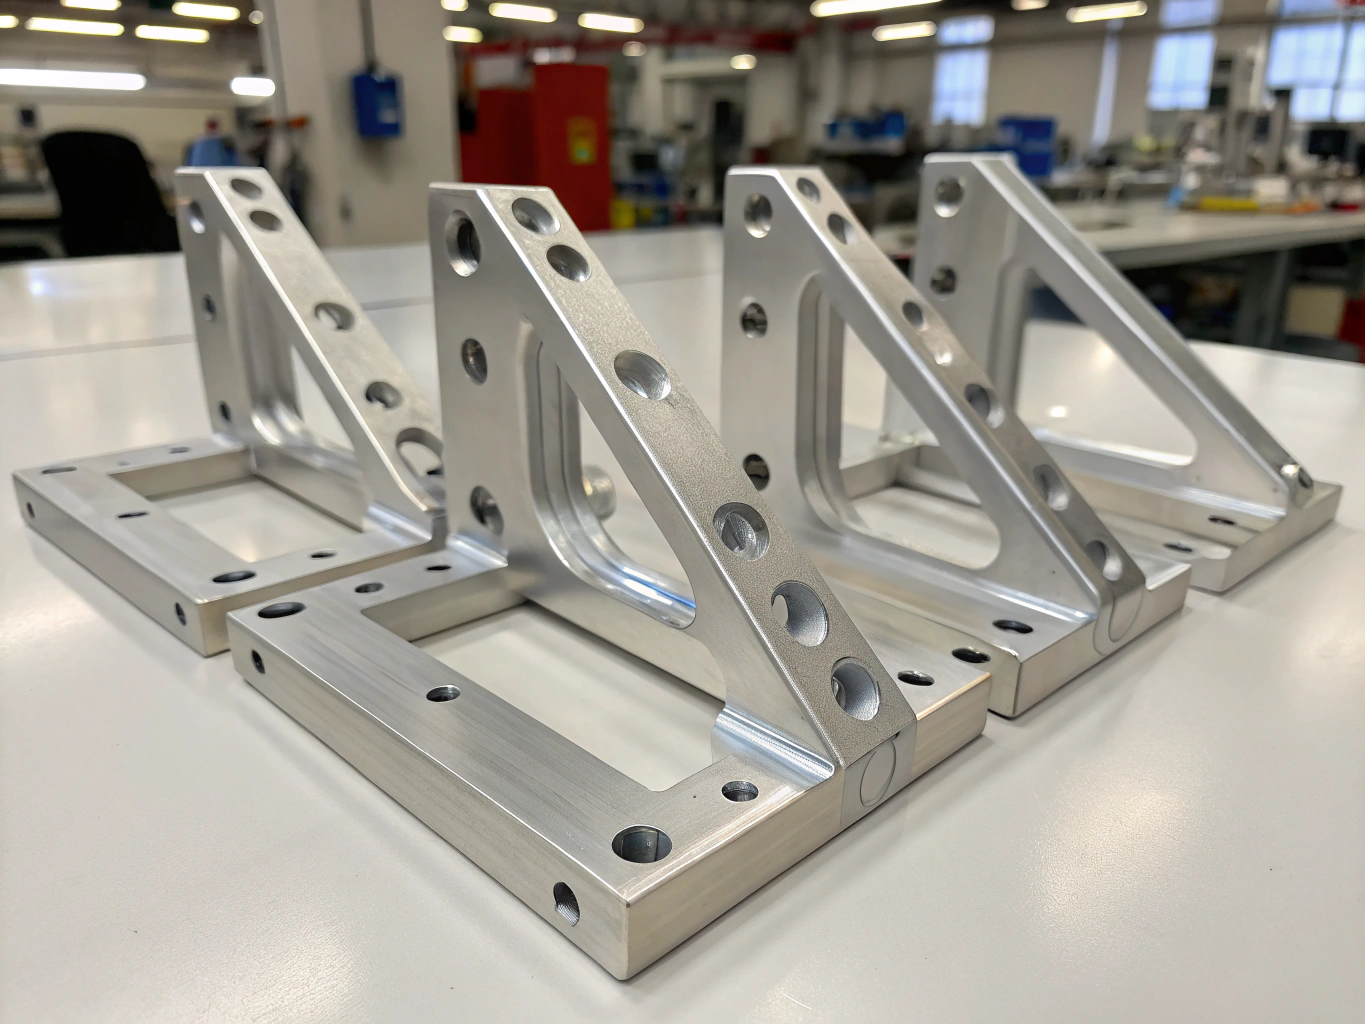
Typical Materials
High-Strength Low-Alloy (HSLA) Steel, 6061-T6 Aluminum
Finishes & Quality
E-Coat (KTL), Zinc-Nickel Electroplating
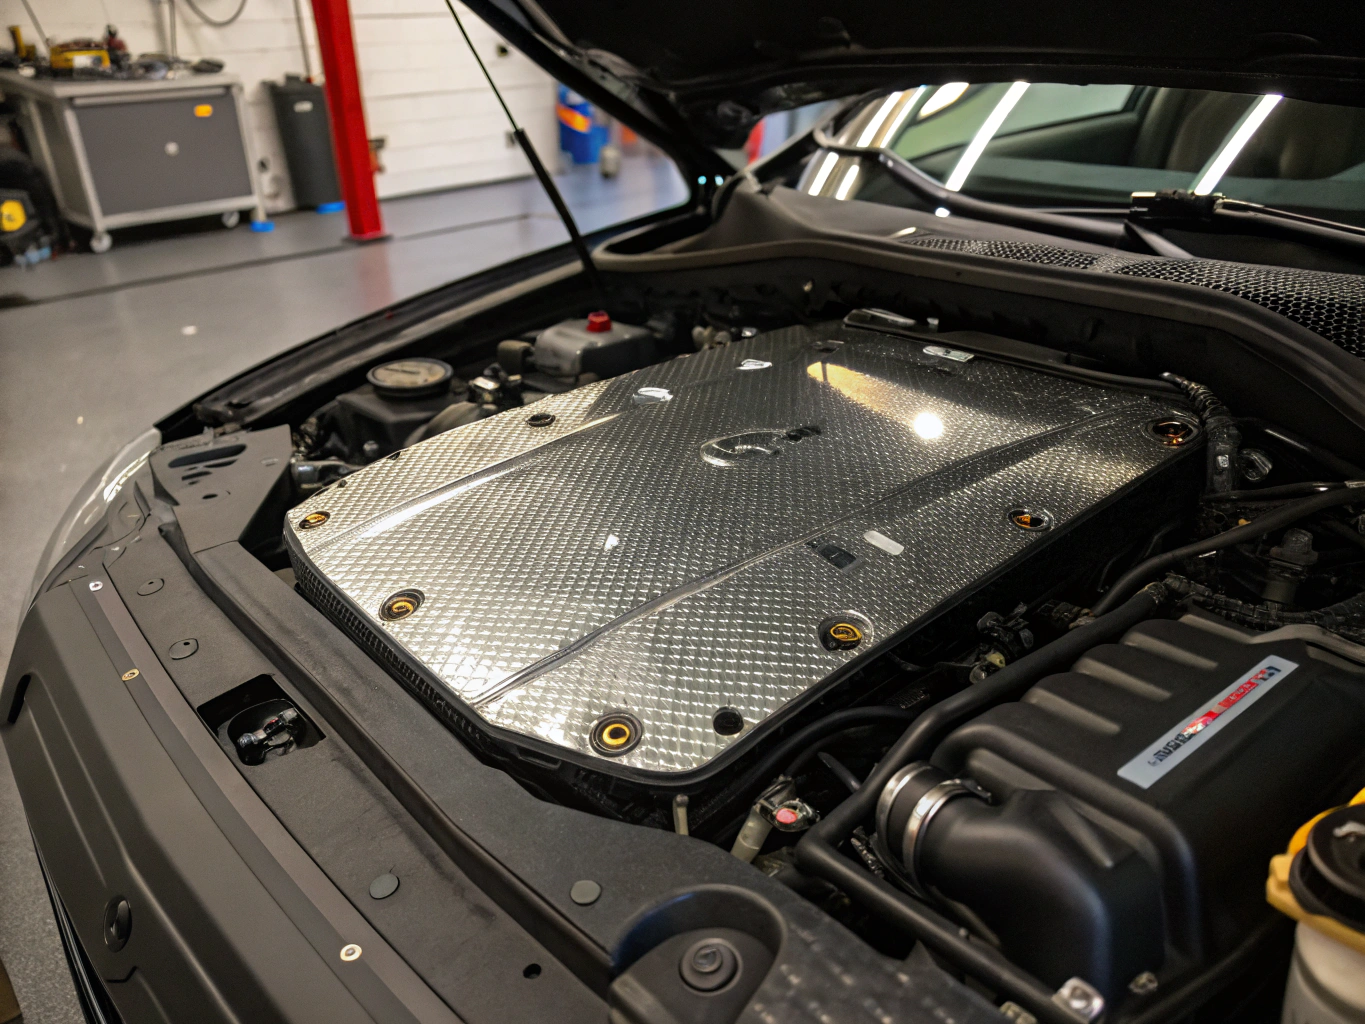
Typical Materials
Aluminized Steel 409/304, Embossed 1050/3003 Aluminum
Finishes & Quality
Micro-Embossing, Ceramic Thermal Barrier Coatings
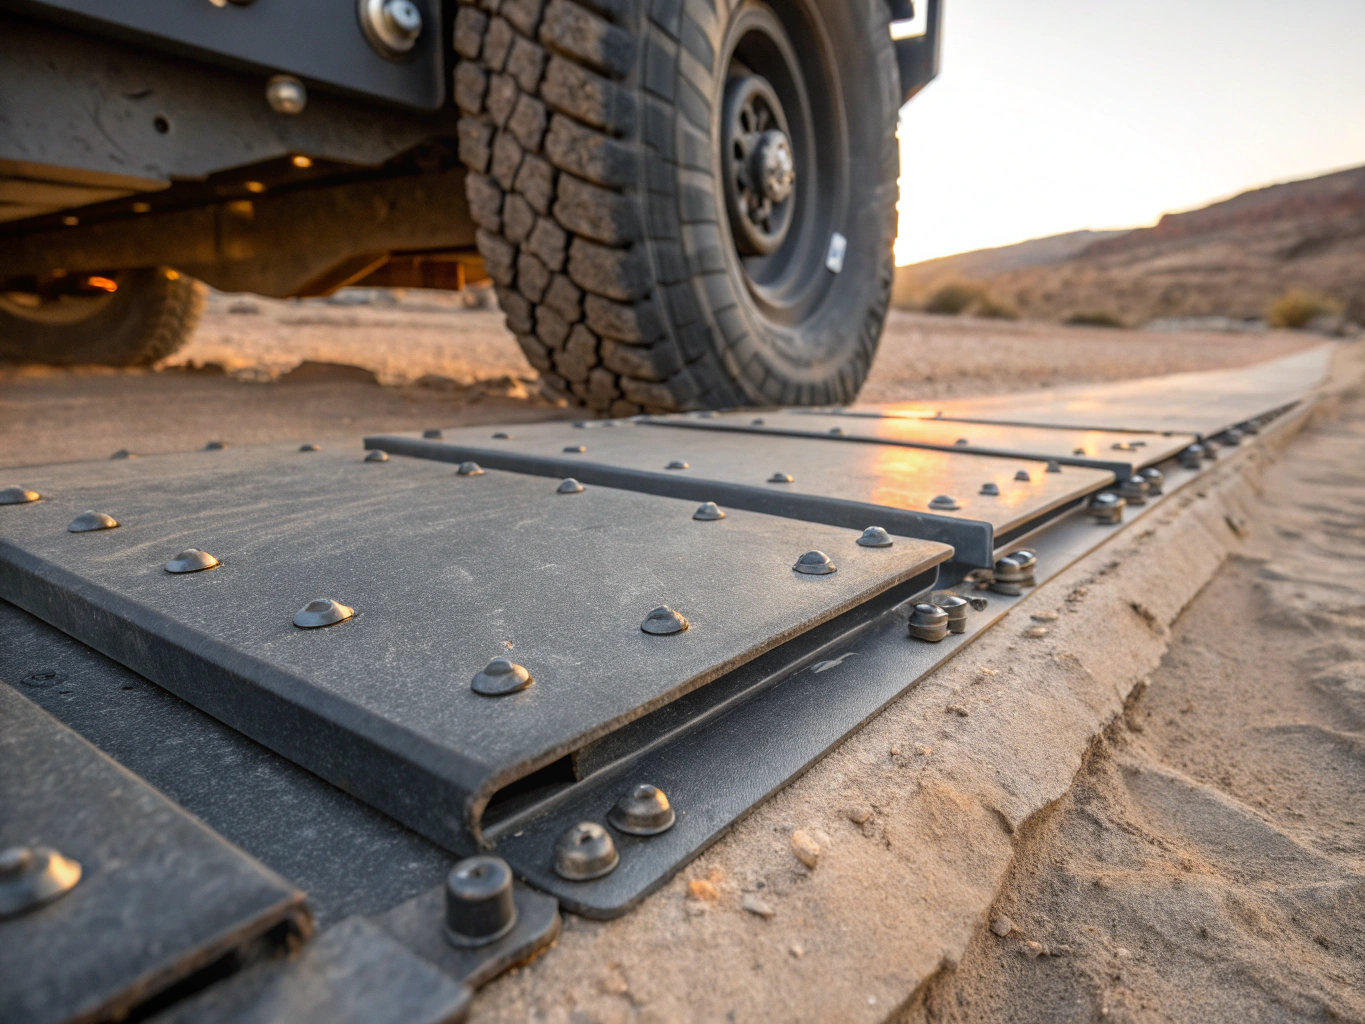
Typical Materials
5052-H32 / 5083 Aluminum (4-8mm), High-Yield Q345B Steel
Finishes & Quality
Architectural Grade Powder Coating, Hard Anodizing
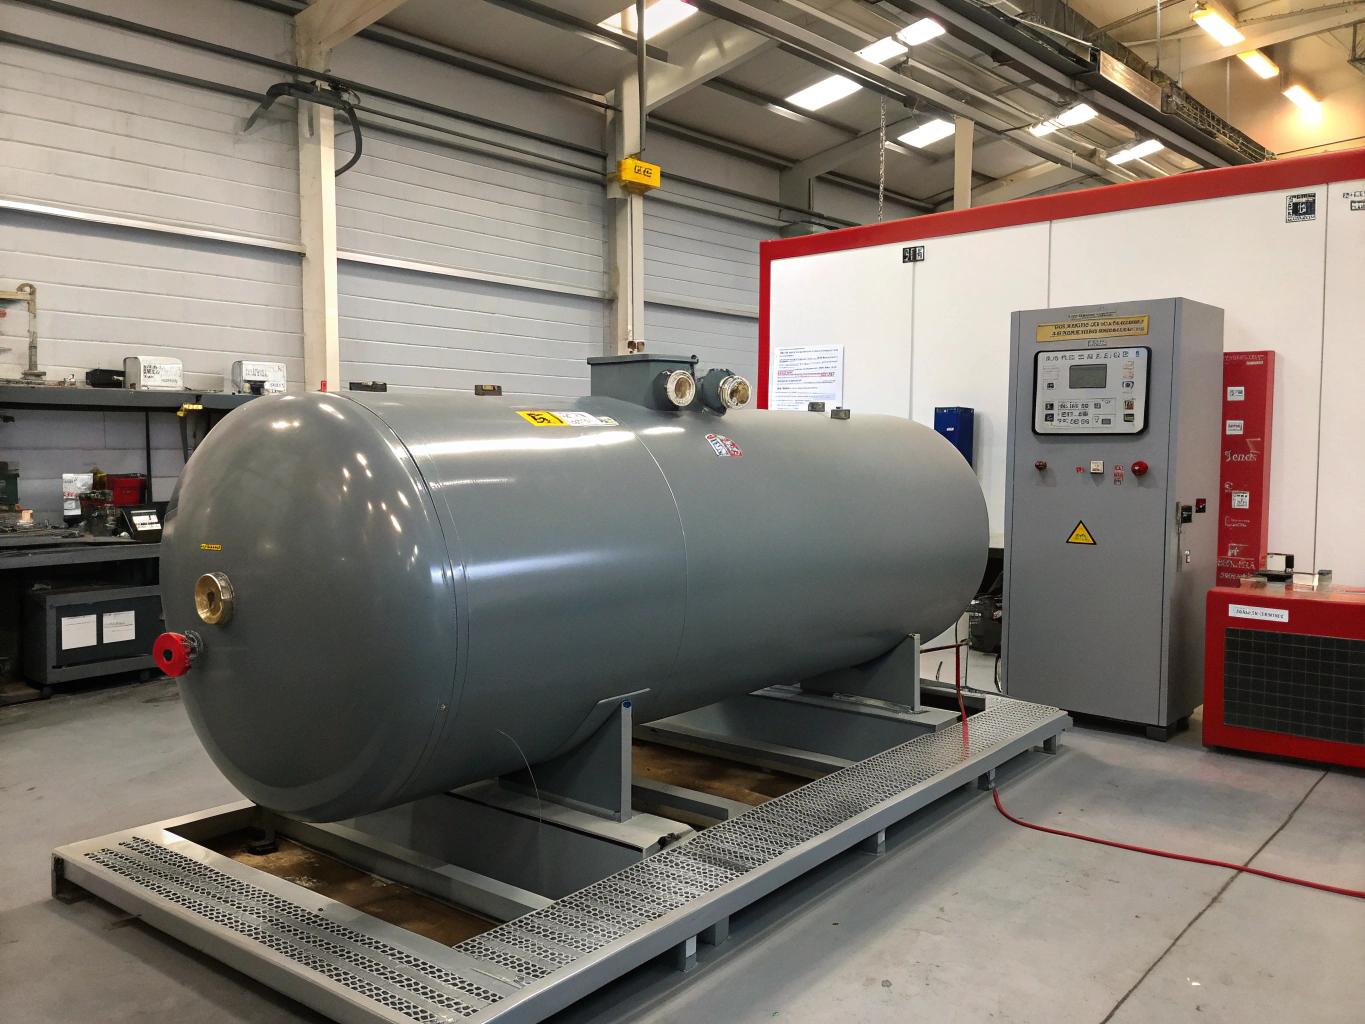
Typical Materials
5052 / 6061 Aluminum Alloy, 304L Stainless Steel
Finishes & Quality
Internal Passivation, Anodizing, Hydrostatic Pressure Testing
Typical Materials
Cold Rolled Steel (SPCC/DC01), 3003-H14 Aluminum
Finishes & Quality
Electrostatic Powder Coating, Anti-Corrosion Primer
Custom automotive stampings & OEM assemblies
Send your CAD drawings (STEP, IGES, DXF) for DFM analysis and precision contract manufacturing quotes.
How your parts are built from sheet to spec
A controlled five-stage workflow engineered for tight tolerances, repeatable batch runs, and clean surface finishes.
Stamping & blanking
High-speed CNC fiber lasers and turret punch presses cut flat blanks to precision dimensions with minimal kerf.
Forming & bending
Multi-axis CNC press brakes and automated panel benders form complex geometric angles and deep draws. Related reading: hemming sheet metal edges.
Welding & joining
TIG, MIG, and robotic seam welding combined with automated PEM fastener insertion for structural joints.
Surface finishing
In-house automated powder coating, electroplating, anodizing, and bead blasting for rugged corrosion resistance.
Final QA & assembly
Hexagon CMM coordinate inspection, visual checks, hardware assembly, and custom export crating.
Need custom tooling or high-volume OEM production?
Send your 2D/3D CAD drawings for a comprehensive DFM review and quotation within 24 hours.
Manufacturing specifications
Review standard material grades, forming limits, dimensional tolerances, and surface treatments for industrial assemblies.
Related reading: countersink and hole sizing.
Engine brackets
Material: Cold-rolled steel / 1018
Thickness: 3.0 mm – 6.0 mm
Surface: E-coat + black powder coat
High fatigue strength and tight hole pitch
Heat shields
Material: Embossed 304 stainless / Al 5052
Thickness: 0.6 mm – 1.2 mm
Surface: Mill / Passivated
Thermal deflection control under 650 deg C
Skid plates
Material: Aluminum 5052-H32 / High-strength steel
Thickness: 4.0 mm – 8.0 mm
Surface: Hard anodize / Heavy textured powder
High impact resistance with countersunk bolt holes
Fluid reservoirs
Material: 304L stainless / 5052 aluminum
Thickness: 1.5 mm – 2.5 mm
Surface: Internal passivate / TIG weld clean
100% pneumatic pressure tested to 0.4 MPa
Louvered panels
Material: Galvannealed steel / Aluminum
Thickness: 1.2 mm – 2.0 mm
Surface: Outdoor polyester powder coat
Formed ventilation slots with uniform airflow gap
| Material type | Thickness range | Laser tolerance | Typical components | Recommended finishing |
|---|---|---|---|---|
| Cold-rolled steel (SPCC / 1018) | 0.5 mm – 6.0 mm (24 ga – 3 ga) | +/- 0.10 mm | Engine brackets, chassis frames, structural mounts | E-coat, powder coat, zinc plating |
| Stainless steel (304 / 316 / 430) | 0.6 mm – 8.0 mm (24 ga – 0 ga) | +/- 0.08 mm | Fluid reservoirs, exhaust heat shields, marine hardware | Passivation, electropolishing, bead blast |
| Aluminum (5052-H32 / 6061-T6) | 0.8 mm – 10.0 mm (20 ga – 3/8 in) | +/- 0.12 mm | Skid plates, louvered panels, lightweight enclosures | Anodizing (Type II & III), chromate conversion |
| Galvannealed steel (A40 / A60) | 0.8 mm – 4.5 mm (22 ga – 7 ga) | +/- 0.10 mm | Outdoor power enclosures, HVAC dampers, plenum boxes | Direct powder coating, wet spray paint |
| Copper & brass (C110 / C260) | 0.5 mm – 5.0 mm (24 ga – 5 ga) | +/- 0.05 mm | Electrical busbars, grounding clips, heat dissipation tabs | Tin plating, silver plating, bright dip |
Need custom tolerances or specialty alloys?
Our engineering team reviews STEP, DXF, and CAD models to verify DFM feasibility within 24 hours.
Related metal fabrication services
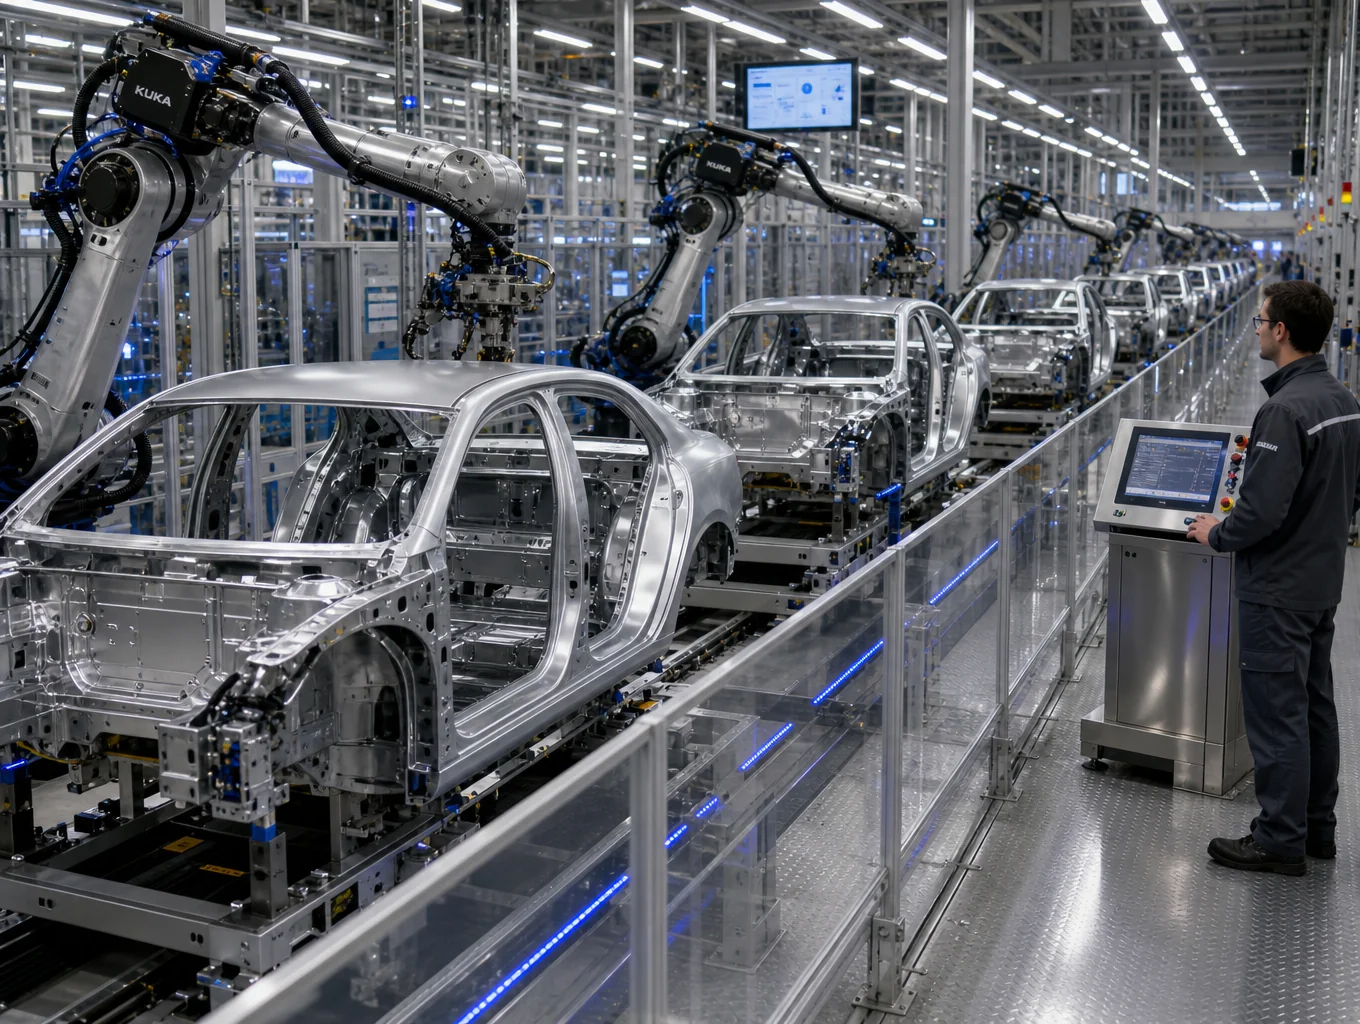
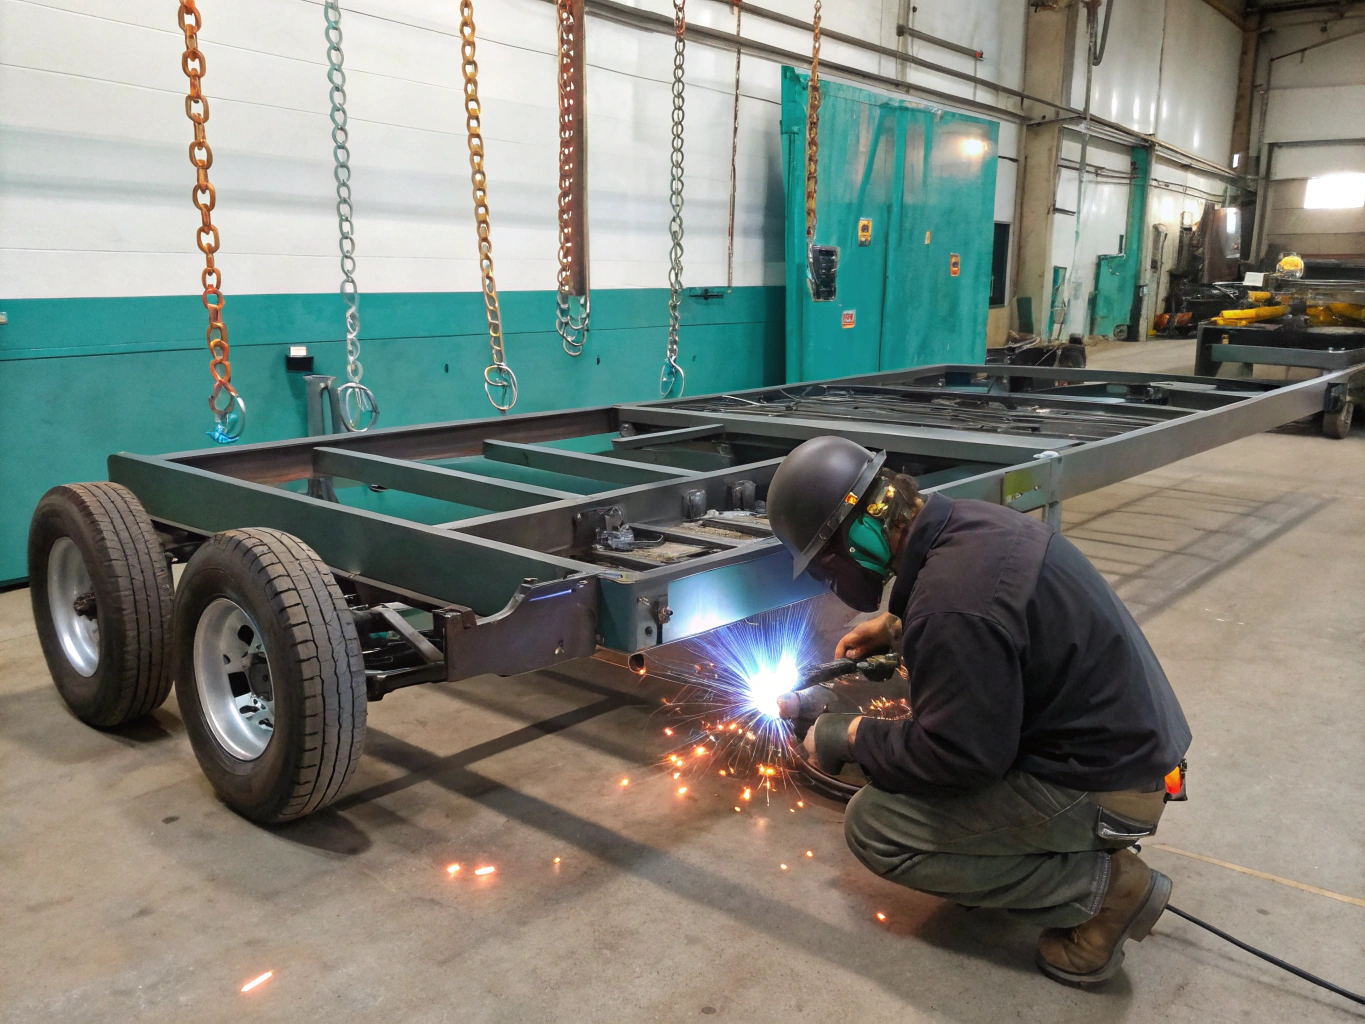
Complementary contract manufacturing solutions for transportation, automotive systems, rivet nuts and threaded fasteners, and mission-critical assemblies.
Request a custom manufacturing quote
Send us your technical drawings or functional hardware specifications. Our engineering team will review your requirements and provide DFM feedback with competitive unit pricing.
24-Hour DFM feedback
Rapid engineering review on tolerances, tooling, and cost optimization.
Strict ISO compliance
Full material certs, CMM dimension reports, and lot traceability.
Global supply delivery
Direct OEM logistics handling customs, crating, and ocean/air freight.
We safeguard all client IP. Contact our sales department directly to exchange formal mutual non-disclosure documents prior to CAD transmission.